Explore our high-performance clinical instruments engineered for supreme safety, precision, and global regulatory compliance.
Pioneering safety medical device manufacturing through cutting-edge automation, rigorous quality control, and unwavering commitment to human health.
Established in May of 2004, Nanjing Seeker Medical Co., Ltd. has evolved into a professional manufacturer specialized in the research, development, and production of surgical sutures and surgical needles. Over two decades of intensive industry experience have enabled us to build robust supply chains and precise manufacturing methodologies that satisfy the most stringent international regulatory frameworks.
All of our products comply with international and interior quality standards, holding official Production licenses alongside CE, ISO13485, ISO14001, and ISO45001 certificates. These certifications reflect our holistic approach to quality management, environmental responsibility, and occupational health and safety across our global manufacturing footprint.
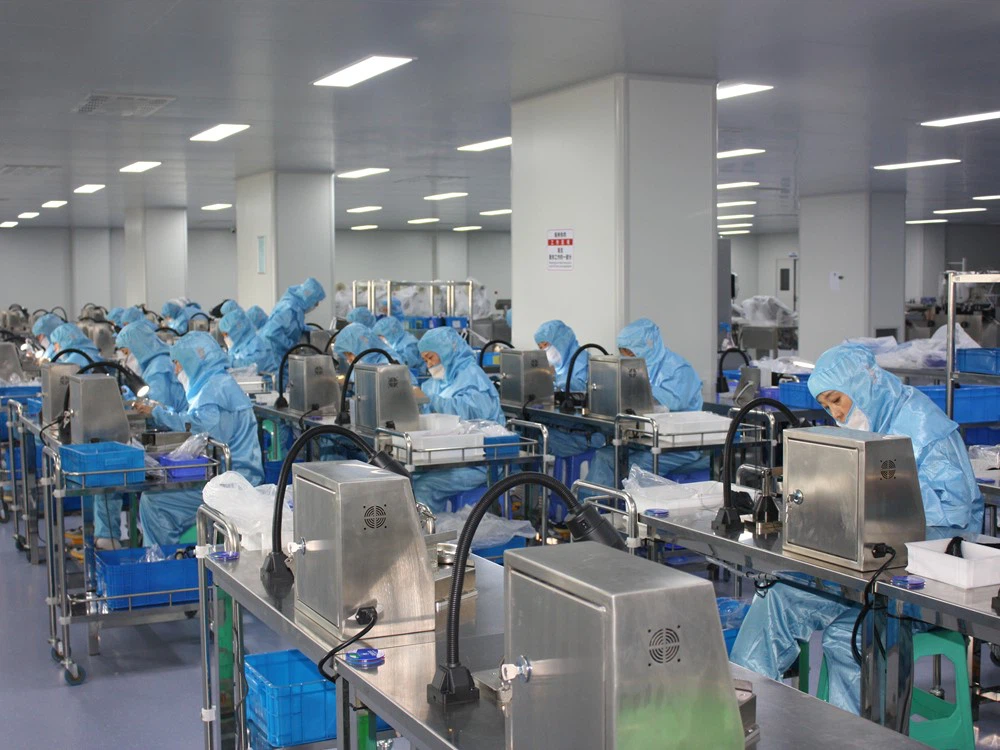
We insist on the quality policy of modern techniques, excellent quality, and customer satisfaction. We attach great importance to the development and application of new technology. So far, we have obtained 29 new invention patents, successfully realizing the automatic transformation of our core production processes.
This automated integration minimizes human error, ensures absolute batch consistency, and scales up production efficiency to meet soaring international demands. Consequently, our innovations and product portfolios are greatly appreciated in a variety of different markets throughout the world, establishing Nanjing Seeker Medical as a trusted OEM/ODM partner for multinational medical corporations.
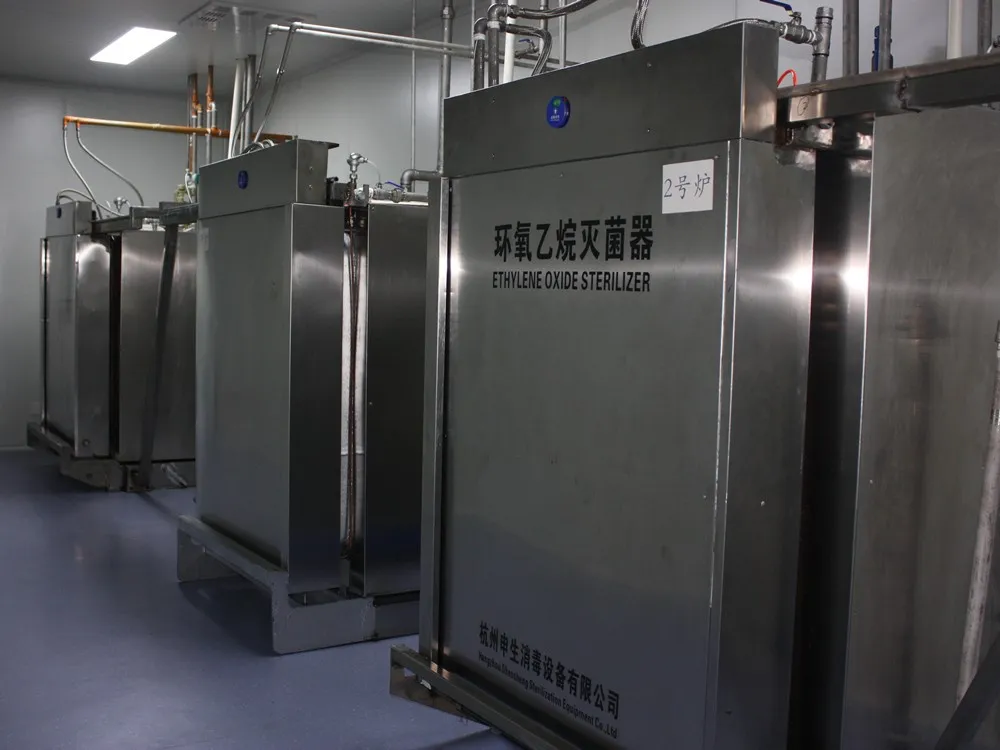
"All staffs in our company welcome every friend from home and abroad. Let us make more efforts for human health career."
An analytical overview of current commercial dynamics, manufacturing efficiencies, and future trends shaping international medical device procurement.
The global demand for safety medical devices has surged exponentially, driven by aging populations, rising chronic disease burdens, and stringent hospital-acquired infection (HAI) prevention protocols. Healthcare systems across North America, Europe, and emerging economies prioritize products featuring sharps-injury protection, sterile barrier integrity, and zero-defect compliance.
China remains the undisputed hub for medical device manufacturing due to integrated supply chain clusters, advanced cleanroom infrastructure, and rapid prototyping capabilities. Factories like ours leverage automated machinery and strict QA protocols to deliver Tier-1 quality at highly competitive cost structures, ensuring optimal ROI for global importers.
The industry is rapidly shifting toward smart medical consumables, eco-friendly biodegradable packaging, and digitized supply chain tracking (UDI compliance). Manufacturers investing in R&D and patented automation are positioned to capture dominant market share in the next decade of healthcare evolution.
Discover our extended range of certified medical consumables, surgical accessories, and diagnostic instruments tailored for clinical excellence.
Expert answers regarding our CE certification, manufacturing standards, and global export capabilities.
 Seeker Medical